






Related Posts
Online Message
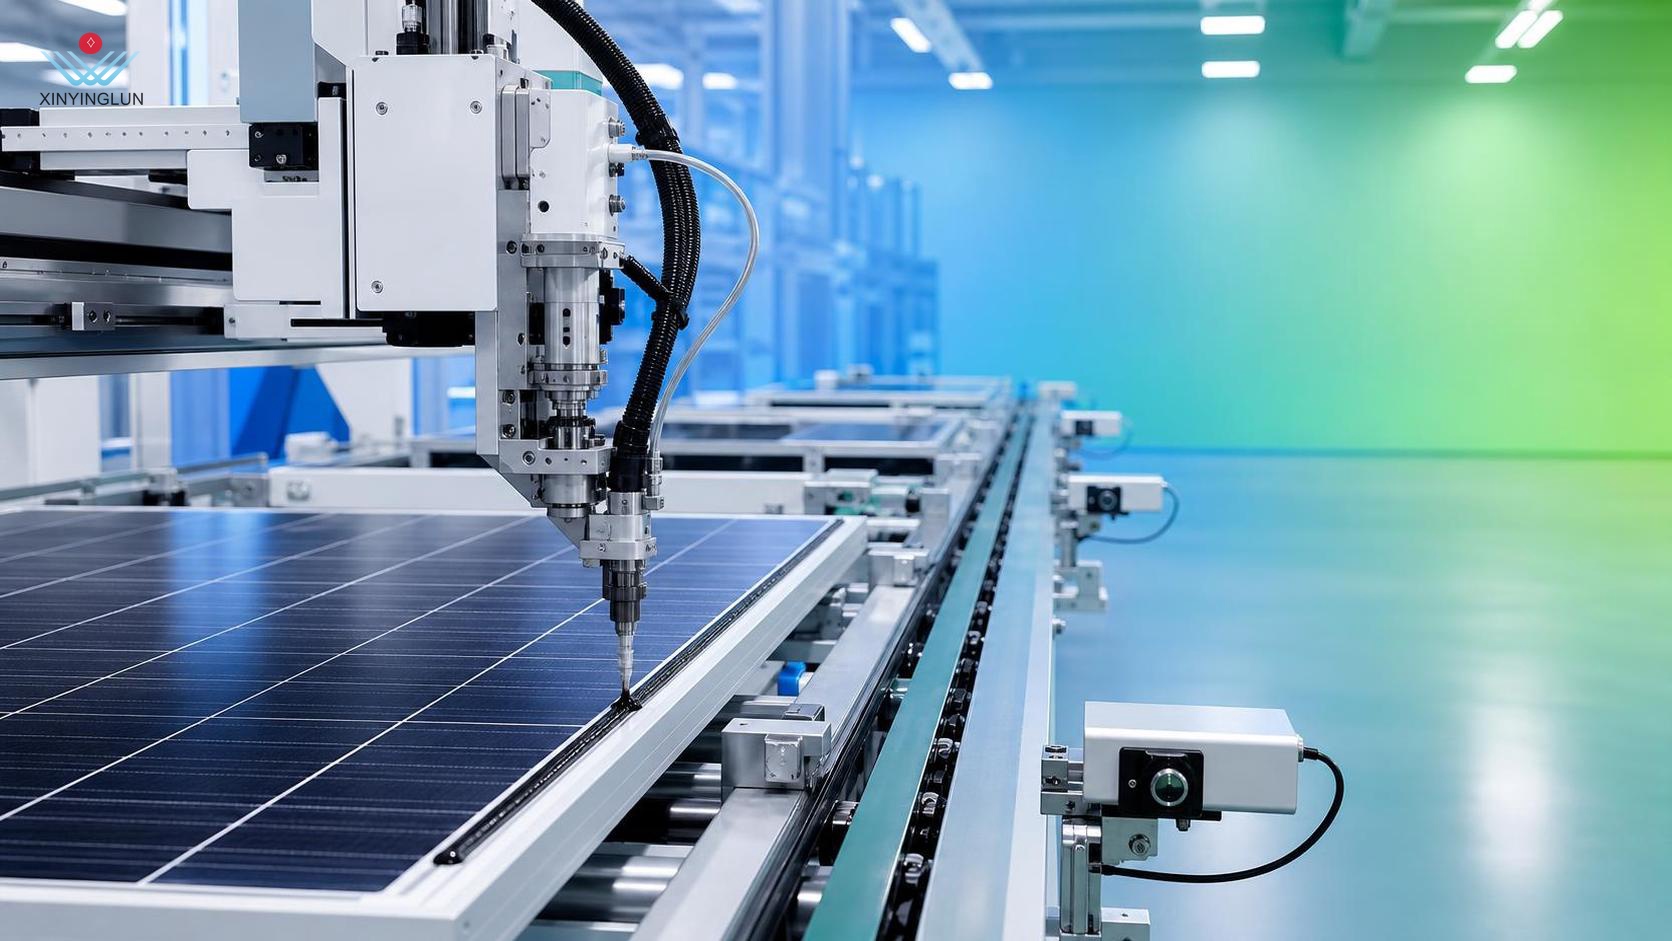
What are common problems with dispensing machines from overseas suppliers? For photovoltaic module manufacturers, the answer is rarely limited to one failed valve or one delayed shipment. The more serious risks often emerge after the equipment reaches the factory: bead width varies from shift to shift, the machine cannot communicate cleanly with the production line, a minor alarm becomes a long shutdown because a spare part is unavailable, or remote support loses value when the supplier cannot see the real process conditions.
Dispensing is a small step in the physical footprint of a PV module line, yet it can have an outsized influence on sealing consistency, material consumption, throughput, and downstream quality. When buying equipment internationally, procurement teams are not simply comparing a machine’s quoted speed or purchase price. They are comparing how much uncertainty each supplier leaves behind.
This comparison looks at the recurring problems with dispensing machines from overseas suppliers, why they matter in photovoltaic manufacturing, and how buyers can distinguish an acceptable procurement risk from a preventable one.
The Difference Between a Machine That Runs and a Process That Stays Stable
A dispensing machine may complete a demonstration successfully and still perform poorly in a production environment. This is one of the most common misunderstandings in cross-border equipment purchasing. A trial often uses controlled materials, a short runtime, and a simplified product. A PV module factory works with changing ambient conditions, repeated shifts, large production volumes, different frame sizes or module designs, and operators who need reliable recovery procedures when something goes wrong.
The real comparison is not “local supplier versus overseas supplier.” Many overseas manufacturers deliver capable automation systems, and many domestic suppliers can fall short. The meaningful comparison is between a supplier that understands the full dispensing process and one that only sells a configured machine.
1. Dispensing Accuracy That Does Not Hold Through Real Production
In photovoltaic module assembly, an inconsistent adhesive or sealant bead can create more than a cosmetic defect. Depending on the application, it may affect bonding performance, sealing continuity, material use, rework rates, and confidence in long-term module reliability. The problem is not always obvious at the machine exit. A bead can appear acceptable to the eye while varying in volume, placement, or corner coverage enough to cause later concerns.
Some overseas quotations describe accuracy in broad terms without explaining the test method. Was the result measured on a flat plate or an actual module component? Was the dispense material at normal production viscosity? How long had the system been operating before the measurement? These questions matter because pumps, valves, hoses, temperature conditions, pressure settings, and motion parameters all influence the final bead.
Buyers should be cautious when a supplier discusses only the motion platform. Servo control and a rigid frame are important, but they do not alone guarantee stable dispensing. The material delivery system deserves equal attention: pressure control, metering method, valve response, anti-drip behavior, temperature management where relevant, and the ability to maintain a consistent output as material conditions change.
A stronger technical discussion includes representative samples, a defined bead specification, measurement points, acceptable variation, start-stop performance, corners, overlaps, and recovery after an interruption. If the supplier cannot turn “good dispensing” into measurable acceptance criteria, the buyer will struggle to resolve disagreements later.
2. Material Compatibility Gets Treated as an Afterthought
Dispensing equipment is not universally compatible simply because it can move adhesive from a container to a nozzle. Sealants and adhesives used in PV module manufacturing can differ in viscosity, filler content, cure characteristics, moisture sensitivity, and required handling conditions. A system that runs one material smoothly may show unstable output, blocked lines, excessive stringing, or difficult cleaning with another.
This risk becomes sharper when the material supplier, dispensing machine supplier, and module manufacturer are located in different countries. Each party may assume that another party owns the problem. The adhesive supplier may point to settings; the equipment supplier may point to material variation; the factory is left with lost production time and no clear root cause.
Before placing an order, provide the supplier with the intended material’s technical data and ask for a written confirmation of compatibility limits. The discussion should cover container format, feeding arrangement, hose length, filtration, mixing requirements if applicable, nozzle selection, cleaning method, and the consequences of planned material changes. If a factory expects to qualify more than one adhesive or sealant, that should be stated early rather than introduced after installation.
It is also wise to ask what happens during pauses. Can the material remain in the system for a defined period? What shutdown and restart procedure is recommended? A machine that dispenses well during continuous operation but requires lengthy cleaning after ordinary pauses may not suit the actual rhythm of the line.
3. Integration Problems Hidden Behind “Standard Interfaces”
PV module automation is a chain. The dispensing station must receive products correctly, identify the model or recipe, complete the programmed path, exchange status signals, and release the product without becoming a bottleneck. When an overseas supplier says the machine has “standard interfaces,” that phrase is not enough. Standards differ by factory, region, PLC preference, and line architecture.
Typical integration failures include incomplete handshake signals, mismatched conveyor heights, unclear product positioning responsibility, recipe changes that cannot be synchronized, barcode or MES data that cannot be passed reliably, and alarm logic that stops adjacent machines unnecessarily. None of these issues sounds dramatic in a quotation. During commissioning, each one can consume days.
For a standalone machine, this may be manageable. For an inline dispensing system, buyers should request an interface responsibility matrix before fabrication begins. It should show the mechanical handoff points, electrical requirements, communication protocol, required signals, safety interlocks, emergency-stop behavior, product flow direction, and the party responsible for each item.
Cycle time needs the same discipline. A supplier may quote a dispensing time that excludes loading, unloading, vision positioning, material refilling, nozzle cleaning, or error recovery. The line, however, experiences all of them. Ask for a complete cycle-time breakdown for each module format under consideration.
4. Remote Support Is Promised, but Diagnosis Is Too Shallow
Distance changes the meaning of service. When the equipment supplier is overseas, a capable remote-support system can be extremely valuable. But “remote support available” is not a service plan by itself.
Common gaps include time-zone delays, language barriers, no secure remote-access arrangement, incomplete electrical drawings, weak alarm history, and technicians who understand controls but not dispensing behavior. A production manager may send photos and videos for several days while the actual issue—a pressure fluctuation, nozzle wear pattern, sensor position, or recipe logic error—remains unresolved.
Support quality depends on what the supplier can observe. A machine with usable alarm logs, trend data, recipe backup, component identification, and clear documentation is much easier to troubleshoot across borders. During supplier evaluation, ask how a fault is handled from the first call to escalation. Who responds? What information will they request? Can they review PLC or HMI data remotely? When is an on-site visit considered necessary, and who provides it?
The buyer also has responsibilities. The factory should appoint trained maintenance and process contacts, preserve backups of approved recipes, and establish a practical communication route before a breakdown occurs. Remote service becomes more effective when both sides use the same language for symptoms, settings, and acceptance standards.
5. Spare Parts Delays Turn Small Faults Into Major Downtime
A dispensing cell contains components that wear or require periodic replacement: nozzles, seals, hoses, filters, sensors, valves, pumps, fittings, and control parts. A machine can be technically sound yet still become a production liability if a critical component must travel internationally every time it fails.
The most frustrating situations are often avoidable. The supplier may have a spare-parts list, but it is generic and does not identify which parts are critical to restarting production. Or the list uses internal part numbers without a clear description, making urgent ordering difficult. In some cases, the buyer discovers that a commonly used component has an unexpectedly long delivery lead time only after commissioning.
Instead of asking only, “Do you provide spare parts?” ask for three categories: commissioning spares, recommended two-year operating spares, and long-lead critical spares. Each item should include a part number, description, quantity, maintenance purpose, and expected lead time. Where appropriate, confirm whether locally obtainable equivalents are acceptable or whether using alternatives would affect warranty, performance, or calibration.
For high-utilization PV lines, keeping a modest critical-spares inventory is not wasteful purchasing. It is a decision to protect production continuity.
6. Documentation, Wiring Practices, and Safety Expectations May Not Match the Site
Documentation is often underestimated because it does not move material or produce modules. Yet it becomes essential when an operator needs to change a recipe, a maintenance technician traces a sensor fault, or an engineer tries to modify the line years after installation.
Problems may include drawings that do not match the delivered machine, unclear electrical labels, untranslated HMI messages, incomplete pneumatic diagrams, missing preventive-maintenance instructions, or software backups that were never formally handed over. These are not merely administrative inconveniences. They extend troubleshooting time and make the factory more dependent on the original supplier.
Safety alignment also requires an early review. Emergency-stop arrangements, guarding, interlocks, electrical specifications, pneumatic requirements, and local compliance expectations should be considered during design, not after shipment. Retrofitting guards or reworking a control cabinet on site is slower and more expensive than incorporating requirements into the approved layout.
Request documentation as a deliverable with a defined language and format. At minimum, the package should cover layout drawings, utility requirements, electrical and pneumatic schematics, operating instructions, maintenance schedules, spare-parts information, approved process recipes where applicable, and software backup procedures.
7. Quality Claims Are Not Connected to Factory Acceptance
Another common issue with dispensing machines from overseas suppliers is ambiguity around quality control. A supplier may state that equipment is inspected before shipment, but the buyer needs to know what was actually inspected and against which criteria.
A meaningful factory acceptance test should reflect the intended production application as closely as possible. It can include mechanical operation, safety checks, axis movement, dispense path verification, sample evaluation, alarm tests, interface simulation, recipe switching, and repeatability checks. The purpose is not to demand perfection in a supplier’s workshop. It is to make expectations visible while changes are still easier to implement.
Acceptance criteria should be agreed before the test, not negotiated after a problem appears. For example, the buyer may define the product type, material or equivalent test material, required path, bead dimensions, inspection method, cycle-time basis, and conditions that count as a failed test. A short, precise acceptance document is more useful than a broad promise of performance.
How to Compare Overseas Suppliers More Fairly
A low quotation can look compelling when equipment specifications appear similar. Yet the price comparison becomes misleading if one proposal includes on-site commissioning support, complete documents, critical spares, tested line interfaces, and process validation while another treats these as future extras.
Build a comparison sheet that separates the machine price from the cost of uncertainty. Include scope boundaries, installation support, software access, spare parts, training, material compatibility, FAT requirements, remote-service method, and likely lead times for replacement components. This gives engineering, procurement, and production teams a common basis for discussion.
For Chinese PV module manufacturers and international buyers seeking automation equipment, suppliers with a long-term focus on photovoltaic applications can offer a practical advantage: they are more likely to understand that dispensing performance must coexist with line rhythm, module quality control, and maintainability. Shandong XINYINGLUN Intelligent Equipment, for example, develops photovoltaic module automation equipment with an emphasis on manufacturing quality control and technical innovation. The key for any buyer is to convert that stated capability into a reviewable project scope, test plan, and support commitment.
Questions Worth Asking Before the Purchase Order
- Can you demonstrate the proposed configuration using our module dimensions and intended dispensing material, or a clearly defined equivalent?
- What measurable bead-quality and repeatability criteria will be included in the factory acceptance test?
- Which interfaces are included, and what signals, protocols, and responsibilities remain on our side?
- What is included in the stated cycle time: dispensing only, or the complete station cycle?
- Which components should we stock locally to avoid extended downtime?
- How will remote troubleshooting work in practice, including access, language, response route, and escalation?
- Will we receive editable drawings, approved software backups, and a complete maintenance package?
- What process changes require supplier involvement after installation, such as a new frame size, adhesive grade, or module design?
Overseas sourcing does not need to be a gamble. The strongest purchasing decisions are made when teams look beyond the equipment brochure and examine the full operating relationship: process stability, integration ownership, service readiness, spare-parts planning, and measurable acceptance. A dispensing machine should not only perform on the day it arrives. It should remain understandable, maintainable, and stable when the production schedule is under pressure.
Please give us a message